01 / TRACKING
Inventory Tracking
Capture product activity through compatible sensing technologies and connected systems to help operators maintain better visibility into stock movement.
INVENTORY INTELLIGENCE · SMART STORAGE
Turn commercial equipment into a smarter, more connected operation with inventory tracking, intelligent sensing, and automated visibility into product movement.
Scallix helps businesses, equipment operators, and OEM manufacturers explore smart technology for commercial refrigeration, vending equipment, cabinets, storage systems, and other compatible applications.
FROM EQUIPMENT TO INTELLIGENCE
Inventory management becomes more difficult when products are distributed across multiple locations, storage units, vending machines, or commercial equipment.
Smart inventory tracking can help operators understand product movement, monitor stock levels, identify discrepancies, and make replenishment decisions using more timely information.
Scallix focuses on connecting physical equipment with sensing and software capabilities that help turn product activity into useful operational information.
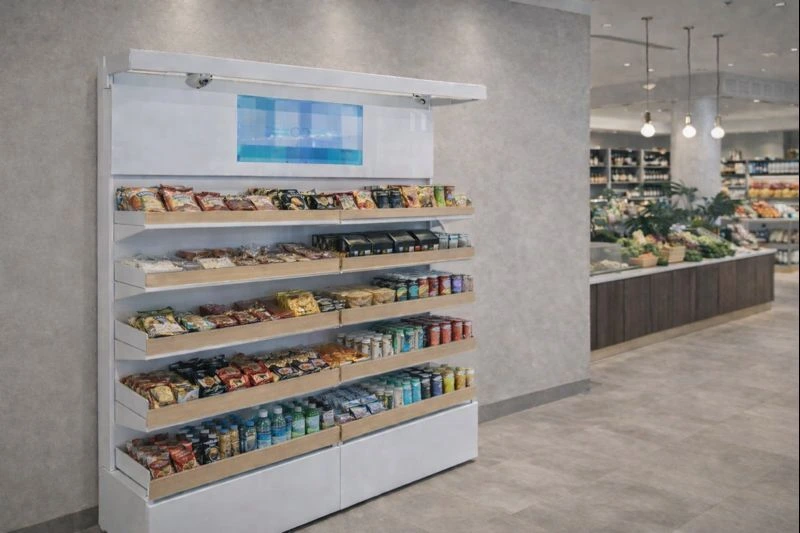
CONNECTED INVENTORY MANAGEMENT
The right inventory tracking solution depends on the equipment, products, operating environment, and level of visibility required. Explore capabilities that can support more informed day-to-day operations.
Capture product activity through compatible sensing technologies and connected systems to help operators maintain better visibility into stock movement.
Review available inventory and operational information remotely, helping teams prioritize replenishment and investigate discrepancies.
Explore technology integrations for compatible cabinets, commercial refrigerators, smart coolers, storage units, and other commercial equipment.
Weight-based sensing can detect measurable changes as products are added or removed, supporting inventory applications where the equipment and products are suitable.
Connected inventory data can help reduce repetitive manual processes and support more consistent operational workflows, depending on system integration.
Equipment manufacturers can explore integrating sensors, connected technology, and inventory intelligence into their own products and equipment platforms.
SMART STORAGE SOLUTIONS
Smart storage is not limited to a single type of cabinet or machine. Depending on the application, sensors and connected technology can help equipment owners gain greater visibility into the products stored inside.
Scallix works with businesses and equipment partners to explore solutions that fit the physical design, operating requirements, and intended use of their equipment.
POTENTIAL OPERATIONAL BENEFITS
BUILT FOR EQUIPMENT OPERATORS & OEMS
Whether you operate commercial equipment or manufacture it, inventory tracking technology can be considered as part of a broader equipment upgrade or product development strategy.
Evaluate whether compatible existing equipment can be upgraded with sensing and connected technology to support inventory monitoring or unattended retail.
Explore integrating inventory sensing into equipment designed and manufactured by your company, subject to technical feasibility and project requirements.
Assess potential sensor configurations and connected capabilities for new equipment concepts, modular products, and specialized commercial applications.
PRIVACY-BY-DESIGN
Some environments have strict requirements governing surveillance cameras, facial recognition, biometric identification, and the collection of personal information. In these locations, the technology used to monitor products can be an important part of the solution design.
Scallix smart cooler technology uses weight-based product recognition in compatible configurations. This allows the system to recognize product activity through measurable weight changes without requiring cameras to identify products.
This approach may be worth considering for healthcare facilities, universities, secure workplaces, government facilities, and other environments where privacy requirements influence technology decisions.
Privacy suitability depends on the complete deployment, including payment processing, access controls, connected software, and the facility's own policies. These requirements should be reviewed before implementation.
A MORE PRIVACY-CONSCIOUS APPROACH
APPLICATIONS
Different businesses have different inventory challenges. Smart sensing and connected equipment can be explored wherever product visibility, replenishment, or unattended access is important.
FROM REQUIREMENTS TO INTEGRATION
Successful inventory tracking starts with understanding the equipment and the information your operation needs.
Identify the equipment, products, locations, and inventory challenges you want to address.
Review equipment design, product characteristics, sensor requirements, and technical constraints.
Establish inventory reporting needs and review the privacy, security, and data-handling requirements.
Determine the appropriate configuration and integration approach for your intended operating environment.
EXPLORE SCALLIX
Explore our smart cooler technology, review retrofit possibilities, or estimate the potential business case for your project.
FREQUENTLY ASKED QUESTIONS
Learn more about inventory tracking integration, smart storage, weight-based sensing, equipment compatibility, and privacy.
Inventory tracking technology helps businesses monitor product quantities and movement. Depending on the solution, it can use sensors, connected equipment, software, and transaction data to improve inventory visibility and support replenishment decisions.
Smart storage solutions combine physical storage equipment with sensing, connectivity, or software capabilities. Depending on the application, these systems can help monitor product movement, improve inventory visibility, and support more informed operational decisions.
Some existing equipment may be suitable for a retrofit. Compatibility depends on its construction, dimensions, operating conditions, products, and the intended technology configuration. Scallix can help review potential options for compatible equipment.
Weight-based sensing measures changes in weight as products are added or removed. When the products, equipment, and system configuration are suitable, these measurements can support product recognition and inventory updates.
Not always. Compatible weight-based systems can recognize product activity without requiring cameras for product recognition. The appropriate technology depends on the equipment, products, operating requirements, and the information the system needs to capture.
Weight-based product recognition may be suitable for locations that restrict camera-based product identification or facial recognition. The full system must still be reviewed against the site's policies, including payment processing, data handling, and access control.
Equipment manufacturers can explore integrating sensing and connected technology into compatible products. Feasibility depends on the product's design, technical requirements, expected use, and the desired inventory monitoring capabilities.
Remote inventory visibility may be available when the selected equipment, sensors, connectivity, and software support it. The available reporting, alerts, and monitoring features depend on the specific configuration.
You can use the Scallix ROI Generator to explore potential revenue and payback based on your own assumptions. Actual results depend on the equipment, application, sales, operating costs, and implementation requirements.
MAKE YOUR EQUIPMENT SMARTER
Tell us about your equipment, products, inventory challenges, and integration goals. We'll help you explore the right Scallix solution for your application.
INVENTORY INTELLIGENCE · SMART STORAGE
Turn commercial equipment into a smarter, more connected operation with inventory tracking, intelligent sensing, and automated visibility into product movement.
Scallix helps businesses, equipment operators, and OEM manufacturers explore smart technology for commercial refrigeration, vending equipment, cabinets, storage systems, and other compatible applications.
FROM EQUIPMENT TO INTELLIGENCE
Inventory management becomes more difficult when products are distributed across multiple locations, storage units, vending machines, or commercial equipment.
Smart inventory tracking can help operators understand product movement, monitor stock levels, identify discrepancies, and make replenishment decisions using more timely information.
Scallix focuses on connecting physical equipment with sensing and software capabilities that help turn product activity into useful operational information.
CONNECTED INVENTORY MANAGEMENT
The right inventory tracking solution depends on the equipment, products, operating environment, and level of visibility required. Explore capabilities that can support more informed day-to-day operations.
Capture product activity through compatible sensing technologies and connected systems to help operators maintain better visibility into stock movement.
Review available inventory and operational information remotely, helping teams prioritize replenishment and investigate discrepancies.
Explore technology integrations for compatible cabinets, commercial refrigerators, smart coolers, storage units, and other commercial equipment.
Weight-based sensing can detect measurable changes as products are added or removed, supporting inventory applications where the equipment and products are suitable.
Connected inventory data can help reduce repetitive manual processes and support more consistent operational workflows, depending on system integration.
Equipment manufacturers can explore integrating sensors, connected technology, and inventory intelligence into their own products and equipment platforms.
SMART STORAGE SOLUTIONS
Smart storage is not limited to a single type of cabinet or machine. Depending on the application, sensors and connected technology can help equipment owners gain greater visibility into the products stored inside.
Scallix works with businesses and equipment partners to explore solutions that fit the physical design, operating requirements, and intended use of their equipment.
POTENTIAL OPERATIONAL BENEFITS
BUILT FOR EQUIPMENT OPERATORS & OEMS
Whether you operate commercial equipment or manufacture it, inventory tracking technology can be considered as part of a broader equipment upgrade or product development strategy.
Evaluate whether compatible existing equipment can be upgraded with sensing and connected technology to support inventory monitoring or unattended retail.
Explore integrating inventory sensing into equipment designed and manufactured by your company, subject to technical feasibility and project requirements.
Assess potential sensor configurations and connected capabilities for new equipment concepts, modular products, and specialized commercial applications.
PRIVACY-BY-DESIGN
Some environments have strict requirements governing surveillance cameras, facial recognition, biometric identification, and the collection of personal information. In these locations, the technology used to monitor products can be an important part of the solution design.
Scallix smart cooler technology uses weight-based product recognition in compatible configurations. This allows the system to recognize product activity through measurable weight changes without requiring cameras to identify products.
This approach may be worth considering for healthcare facilities, universities, secure workplaces, government facilities, and other environments where privacy requirements influence technology decisions.
Privacy suitability depends on the complete deployment, including payment processing, access controls, connected software, and the facility's own policies. These requirements should be reviewed before implementation.
A MORE PRIVACY-CONSCIOUS APPROACH
APPLICATIONS
Different businesses have different inventory challenges. Smart sensing and connected equipment can be explored wherever product visibility, replenishment, or unattended access is important.
FROM REQUIREMENTS TO INTEGRATION
Successful inventory tracking starts with understanding the equipment and the information your operation needs.
Identify the equipment, products, locations, and inventory challenges you want to address.
Review equipment design, product characteristics, sensor requirements, and technical constraints.
Establish inventory reporting needs and review the privacy, security, and data-handling requirements.
Determine the appropriate configuration and integration approach for your intended operating environment.
EXPLORE SCALLIX
Explore our smart cooler technology, review retrofit possibilities, or estimate the potential business case for your project.
FREQUENTLY ASKED QUESTIONS
Learn more about inventory tracking integration, smart storage, weight-based sensing, equipment compatibility, and privacy.
Inventory tracking technology helps businesses monitor product quantities and movement. Depending on the solution, it can use sensors, connected equipment, software, and transaction data to improve inventory visibility and support replenishment decisions.
Smart storage solutions combine physical storage equipment with sensing, connectivity, or software capabilities. Depending on the application, these systems can help monitor product movement, improve inventory visibility, and support more informed operational decisions.
Some existing equipment may be suitable for a retrofit. Compatibility depends on its construction, dimensions, operating conditions, products, and the intended technology configuration. Scallix can help review potential options for compatible equipment.
Weight-based sensing measures changes in weight as products are added or removed. When the products, equipment, and system configuration are suitable, these measurements can support product recognition and inventory updates.
Not always. Compatible weight-based systems can recognize product activity without requiring cameras for product recognition. The appropriate technology depends on the equipment, products, operating requirements, and the information the system needs to capture.
Weight-based product recognition may be suitable for locations that restrict camera-based product identification or facial recognition. The full system must still be reviewed against the site's policies, including payment processing, data handling, and access control.
Equipment manufacturers can explore integrating sensing and connected technology into compatible products. Feasibility depends on the product's design, technical requirements, expected use, and the desired inventory monitoring capabilities.
Remote inventory visibility may be available when the selected equipment, sensors, connectivity, and software support it. The available reporting, alerts, and monitoring features depend on the specific configuration.
You can use the Scallix ROI Generator to explore potential revenue and payback based on your own assumptions. Actual results depend on the equipment, application, sales, operating costs, and implementation requirements.
MAKE YOUR EQUIPMENT SMARTER
Tell us about your equipment, products, inventory challenges, and integration goals. We'll help you explore the right Scallix solution for your application.